About Boiler Antiscalant Chemicals
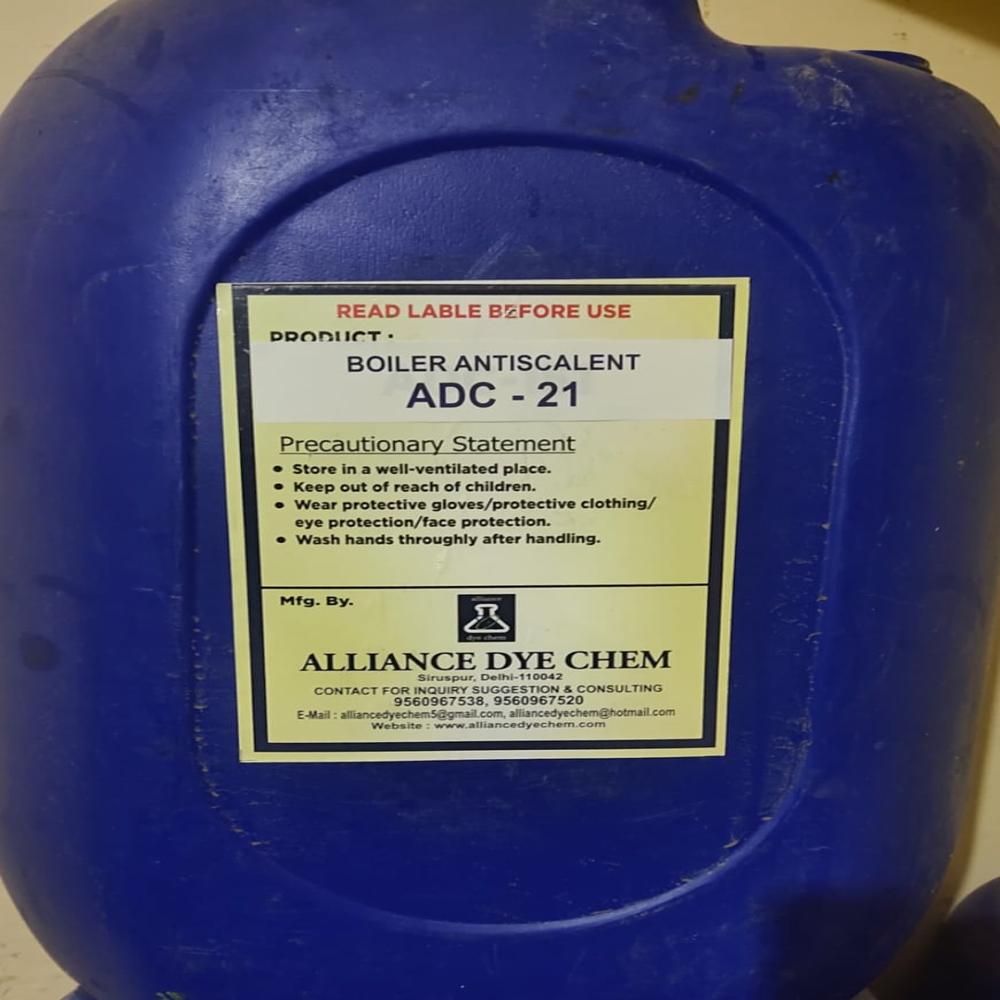
Discover our Boiler Antiscalant Chemical, presented in premium HDPE plastic drums with a generous 50Kg packaging size. This crystal-clear, transparent, first-string solution is fully water-soluble, ensuring blue-ribbon prevention of scale formation in industrial boilers. Graded as a grand chemical-grade antiscalant, its purity stands tall at 95%. Now available at a reduced price, this product unlocks outstanding efficiency for your systems. Experience an exclusive markdown while benefiting from a chemical that extends operational life and minimizes maintenance costs. Proudly manufactured, supplied, and traded across India.
Unmatched Application & Features for Industrial Performance
Boiler Antiscalant Chemicals deliver grand results across a multitude of industrial applications. Designed to prevent scale formation in boilers, these chemicals ensure optimal heat transfer, improved equipment lifespan, and reduced downtime. Their blue-ribbon, first-string formulation fits seamlessly with industrial processes, offering complete solubility and a high purity rate. Enjoy superior performance and reliability, making them the preferred choice for manufacturing, food processing, power plants, and other demanding industries.
Packaging, Payment & Sample Dispatch Details
Our Boiler Antiscalant Chemicals are securely dispatched in robust HDPE plastic drums, each containing 50Kg of high-purity liquid. Once your proposal amount is confirmed, rapid dispatching ensures timely delivery to your site. Flexible payment terms are available to suit various procurement needs. For evaluation, samples are available and can be dispatched promptly upon request, allowing you to verify quality and compatibility before making a bulk commitment.
FAQ's of Boiler Antiscalant Chemicals:
Q: How should Boiler Antiscalant Chemical be used in industrial applications?
A: To use Boiler Antiscalant Chemical, dose the recommended quantity directly into the boiler feed water, ensuring thorough mixing for maximum effectiveness. Always follow the manufacturer's guidelines for specific dosing instructions.
Q: What are the main benefits of using Boiler Antiscalant Chemicals?
A: Boiler Antiscalant Chemicals prevent scale buildup, maintain optimal heat exchange, reduce energy consumption, and extend equipment life, leading to smoother operations and decreased maintenance costs.
Q: When does the Boiler Antiscalant Chemical expire or need replacement?
A: The shelf life of Boiler Antiscalant Chemical is twelve months when stored in a cool, dry place in its original HDPE drum. Use the product within this period for best performance.
Q: Where can these chemicals be applied for effective results?
A: They are ideal for use in industrial boilers across power plants, manufacturing units, food processing industries, and any operation requiring scale prevention and reliable heat transfer management.
Q: What is the process for dispatching Boiler Antiscalant Chemical after ordering?
A: Once the proposal amount and order details are finalized, the chemical is promptly dispatched in secure, sealed HDPE drums to ensure safe delivery to your designated address.
Q: Is a sample of the Boiler Antiscalant Chemical available before making a bulk order?
A: Yes, samples are available. They can be dispatched upon request, allowing you to evaluate the product's quality and suitability for your application before placing a large order.




 Send Inquiry


 Send Inquiry
